Sep . 15, 2025 21:25 Back to list
175QJB Deep Well Submersible Pump-Hebei Aochite|High Efficiency&Customization
Introduction
The 175QJB Deep Well Submersible Pump represents a pinnacle of engineering innovation in water management systems. Engineered to meet the rigorous standards of GB/T2816-2014 and GB/T2818-2014, this pump is a testament to the expertise of Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd. (Chinese: 河北傲驰特给排水设备科技有限公司). This article delves into the product's features, technical specifications, applications, and the company's commitment to quality and customization.
Product Overview
The 175QJB Deep Well Submersible Pump is a specialized water extraction solution designed for deep well applications. Its robust construction and advanced design ensure efficient performance in challenging environments. The pump is ideal for agricultural irrigation, industrial water supply, and municipal water management systems. Hebei Aochite's commitment to OEM processing allows for tailored solutions to meet specific client requirements, ensuring versatility and adaptability.
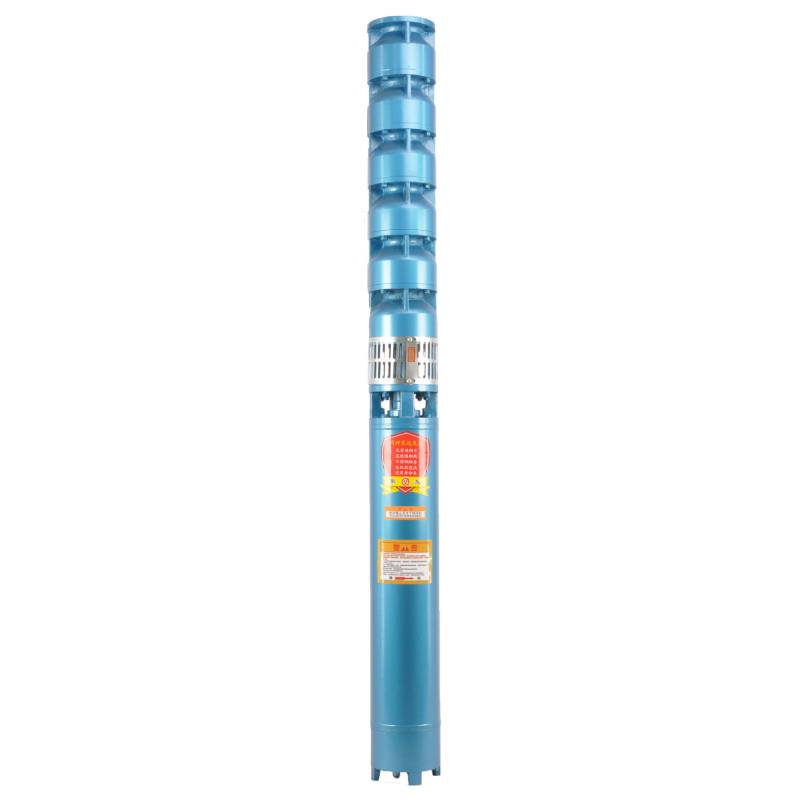
As shown in the image above, the pump's design emphasizes durability and efficiency, with a streamlined body that minimizes resistance and maximizes flow rates. The pump's submersible nature allows it to operate submerged in water, reducing the risk of cavitation and ensuring consistent performance.
Key Features and Advantages
- High Efficiency: The pump is engineered to deliver optimal energy efficiency, reducing operational costs while maintaining high flow rates.
- Durability: Constructed with corrosion-resistant materials, the 175QJB is designed to withstand harsh conditions, ensuring long-term reliability.
- Customization: Hebei Aochite's OEM processing capabilities allow for modifications to meet specific application needs, such as varying depths or water quality requirements.
- Compliance with Standards: Adherence to GB/T2816-2014 and GB/T2818-2014 ensures the pump meets national and international quality benchmarks.
The pump's ability to operate in deep wells makes it a preferred choice for regions with limited surface water access. Its submersible design also reduces the need for complex piping systems, simplifying installation and maintenance.
Technical Specifications
| Parameter | Details |
|---|---|
| Model | 175QJB |
| Power Supply | 380V/50Hz |
| Flow Rate | 10-50 m³/h |
| Head Range | 50-200 meters |
| Material | Cast iron, stainless steel |
| Motor Efficiency | IE3 (High Efficiency) |
| Protection Class | IP68 |
| Operating Temperature | -15°C to 40°C |
For more details, visit the 175QJB Deep Well Submersible Pump product page.
Applications
The 175QJB Deep Well Submersible Pump is versatile, with applications spanning multiple industries:
- Agricultural Irrigation: Efficient water distribution for large-scale farming operations.
- Industrial Water Supply: Reliable water source for manufacturing processes.
- Municipal Use: Supporting water distribution networks in urban areas.
- Groundwater Extraction: Accessing deep aquifers for domestic and commercial use.
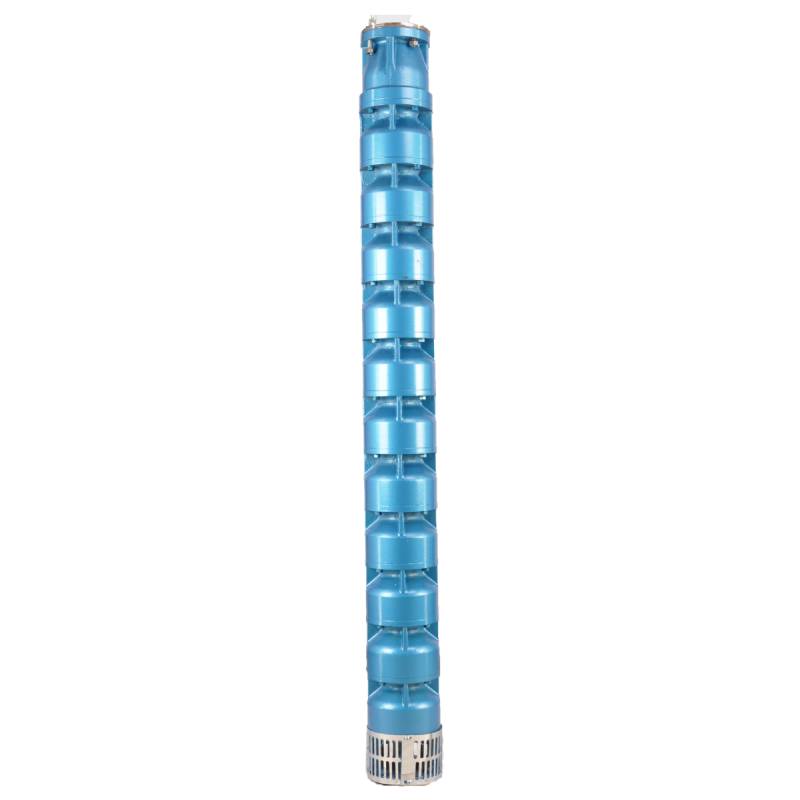
As depicted in the image, the pump is designed for seamless integration into various systems, ensuring minimal downtime and maximum productivity.
Company Background: Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd.
Hebei Aochite is a leading manufacturer specializing in water supply and drainage equipment, with a focus on customized submersible pumps and motors. The company's expertise in OEM processing allows it to cater to diverse client needs, from standard models to highly specialized designs. Hebei Aochite's commitment to quality is reflected in its adherence to GB/T2816-2014 and GB/T2818-2014, ensuring products meet stringent national standards.
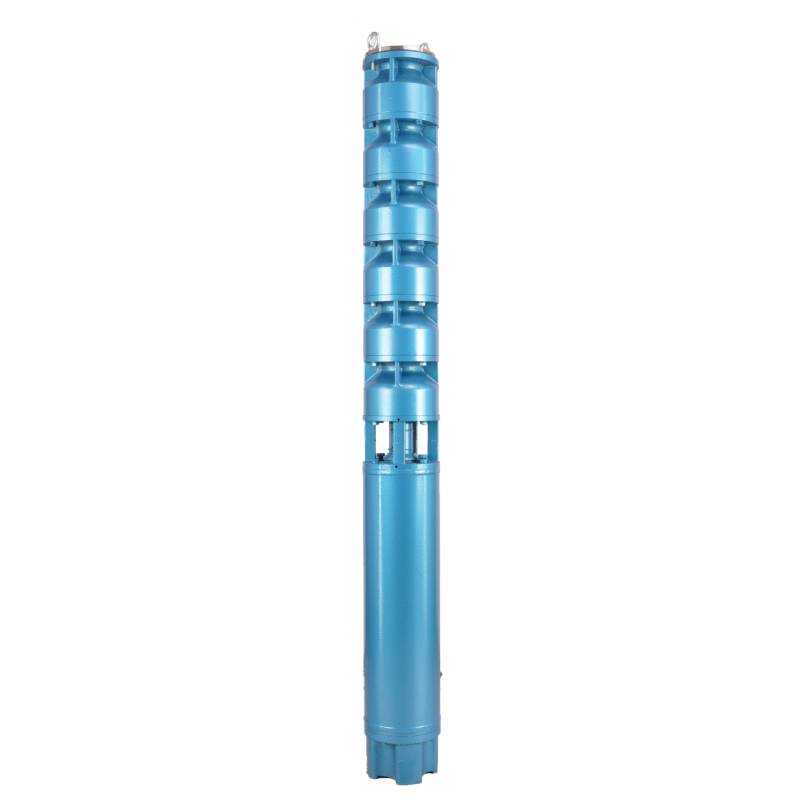
The company's state-of-the-art facilities and skilled workforce enable it to deliver high-quality solutions. For more information about Hebei Aochite, visit their official website.
Industry Standards and Compliance
The 175QJB pump complies with GB/T2816-2014 and GB/T2818-2014, which are critical standards for well submersible pumps and motors in China. These standards ensure that the pump meets requirements for performance, safety, and durability. According to the National Institute of Standards and Technology (NIST), such standards are essential for maintaining consistency and reliability in industrial equipment. 1
For further insights into standards and measurements, visit the NIST website.
Conclusion
The 175QJB Deep Well Submersible Pump is a reliable and efficient solution for deep well water extraction, backed by the expertise of Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd. With its advanced design, compliance with national standards, and customizable features, this pump is an ideal choice for a wide range of applications. Whether for agriculture, industry, or municipal use, the 175QJB delivers exceptional performance and durability.
References
1 National Institute of Standards and Technology (NIST). "Standards and Measurements." https://www.nist.gov
-
Efficient High Performance 1.5 hp deep well water pump Guide
NewsJul.01,2026
-
Choosing the Best 1 hp Vertical Deep Well Pump for Water Supply
NewsJun.29,2026
-
Best 1 hp deep well submersible pump for Water Supply
NewsJun.27,2026
-
Efficient 1 2 hp 5 gpm submersible well pump for Home and Farm
NewsJun.26,2026
-
Best 1 1 2 hp Deep Well Submersible Pump for Water Supply
NewsJun.25,2026
-
Troubleshooting Guide for Submersible Pump Not Working Properly
NewsJun.23,2026
-
 Efficient High Performance 1.5 hp deep well water pump GuideMaximizing Water Efficiency with a 1.5 hp Deep Well Water Pump Finding a reliable water source from deep underground requires precision engineering and robust power. The 1.5 hp deep well water pump offers the perfect balance of energy efficiency and high-performance output for various residential and agricultural needs. Whether you are managing a farm, supplying water to a high-rise building, or ensuring a steady flow for domestic use, selecting the right submersible pump is critical to avoid system failure and costly repairs. In this comprehensive guide, we will explore the technical advantages, installation best practices, and the operational versatility of these specialized pumping systems.Detail
-
 Choosing the Best 1 hp Vertical Deep Well Pump for Water SupplyEnsuring a reliable water supply from deep underground requires precision engineering and the right equipment. The 1 hp vertical deep well pump is a cornerstone for residential and small-scale agricultural water extraction, blending efficiency with powerful lifting capabilities. Whether you are managing a domestic water system, irrigating a garden, or extracting water from a river, selecting a pump with a water-immersed motor ensures long-term durability without water pollution. In this comprehensive guide, we will explore the technical advantages, installation requirements, and maintenance tips to maximize your pumps lifespan.Detail
-
 Best 1 hp deep well submersible pump for Water SupplyChoosing the Best 1 hp Deep Well Submersible Pump for Your Water Needs Finding a reliable water source often requires professional equipment capable of lifting water from significant depths. The 1 hp deep well submersible pump is a versatile and powerful solution designed for residential, agricultural, and industrial applications. By integrating high-quality silicon steel and waterproof motor windings, these pumps ensure longevity and efficiency even in demanding environments. Whether you are managing a farm, supplying a high-rise building, or securing domestic water, understanding the technical nuances of these pumps is key to maximizing your systems lifespan.Detail
 Afrikaans
 Albanian
 Amharic
 Arabic
 Armenian
 Azerbaijani
 Basque
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Catalan
 Cebuano
 Corsican
 Croatian
 Czech
 Danish
 Dutch
 Esperanto
 Estonian
 Finnish
 French
 Frisian
 Galician
 Georgian
 German
 Greek
 Gujarati
 Haitian Creole
 Hausa
 Hawaiian
 Hebrew
 Hindi
 Miao
 Hungarian
 Icelandic
 Igbo
 Indonesian
 Irish
 Italian
 Japanese
 Javanese
 Kannada
 Kazakh
 Khmer
 Rwandese
 Korean
 Kurdish
 Kyrgyz
 Lao
 Latin
 Latvian
 Lithuanian
 Luxembourgish
 Macedonian
 Malgashi
 Malay
 Malayalam
 Maltese
 Maori
 Marathi
 Mongolian
 Myanmar
 Nepali
 Norwegian
 Norwegian
 Occitan
 Pashto
 Persian
 Polish
 Portuguese
 Punjabi
 Romanian
 Russian
 Samoan
 Scottish Gaelic
 Serbian
 Sesotho
 Shona
 Sindhi
 Sinhala
 Slovak
 Slovenian
 Somali
 Spanish
 Sundanese
 Swahili
 Swedish
 Tagalog
 Tajik
 Tamil
 Tatar
 Telugu
 Thai
 Turkish
 Turkmen
 Ukrainian
 Urdu
 Uighur
 Uzbek
 Vietnamese
 Welsh
 Bantu
 Yiddish
 Yoruba
 Zulu
 English