Sep . 08, 2025 16:50 Back to list
175QJB Deep Well Submersible Pump-Hebei Aochite|High Efficiency,Durability
Introduction
The 175QJB Deep Well Submersible Pump represents a cutting-edge solution for water extraction and management in deep well environments. Developed by Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd., this pump is engineered to meet the highest standards of efficiency, durability, and reliability. This article provides an in-depth analysis of the product's features, technical specifications, applications, and the company's commitment to innovation. Additionally, we explore how standards set by organizations like the National Institute of Standards and Technology (NIST) influence the development of such critical equipment.
Product Overview
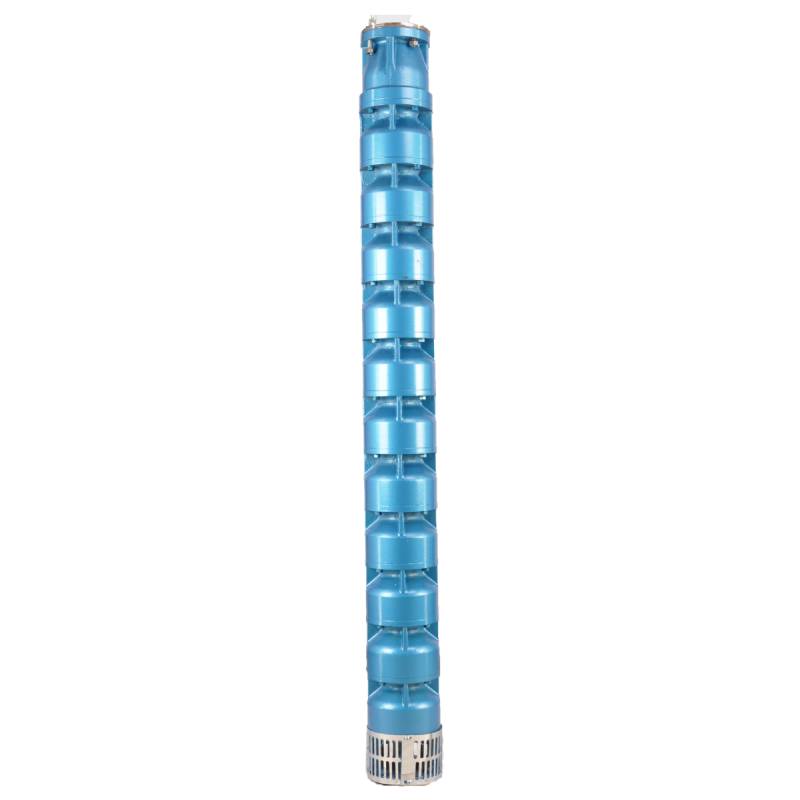
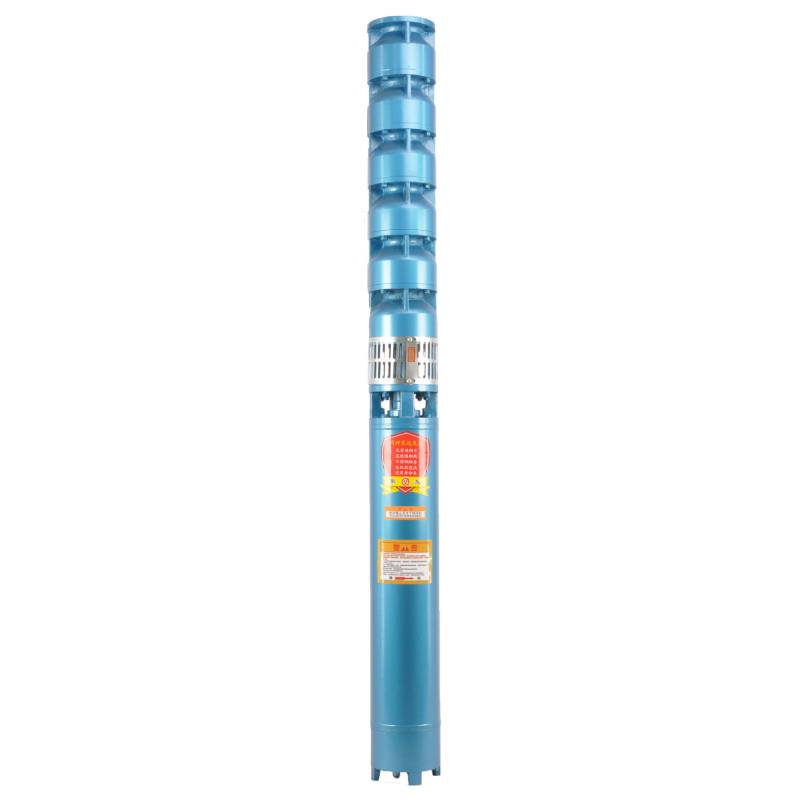
The 175QJB Deep Well Submersible Pump is designed for deep well applications, offering exceptional performance in challenging environments. Its robust construction and advanced engineering make it suitable for both industrial and commercial use. The pump is manufactured under the strict adherence to GB/T 2816-2014 and GB/T 2818-2014 standards, ensuring compliance with national regulations for well submersible pumps and motors. This commitment to quality is a testament to the company's dedication to delivering products that meet global benchmarks.

Key Features and Advantages
1. High Efficiency and Performance
The 175QJB pump is engineered to maximize efficiency, ensuring minimal energy consumption while delivering optimal water flow rates. Its advanced motor design and precision manufacturing reduce operational costs and extend the lifespan of the equipment. This makes it an ideal choice for applications requiring continuous operation, such as agricultural irrigation, industrial cooling systems, and municipal water supply networks.
2. Durability and Reliability
Constructed with high-quality materials, the pump is resistant to corrosion and wear, even in harsh conditions. The use of stainless steel components and sealed bearings ensures long-term performance in deep well environments. This durability is critical for maintaining uninterrupted water supply in remote or challenging locations.
3. Customization and Flexibility
Hebei Aochite specializes in OEM processing, allowing customers to request custom designs tailored to specific requirements. Whether it's adjusting the pump's flow rate, pressure capacity, or integrating it with existing systems, the company's expertise ensures that the product meets the unique needs of each client.
Technical Specifications
| Parameter | Details |
|---|---|
| Model | 175QJB |
| Flow Rate | Varies based on configuration (typically 10-50 m³/h) |
| Head Range | Up to 300 meters |
| Power Rating | 1.5-7.5 kW |
| Motor Type | Submersible asynchronous motor |
| Material | Stainless steel, corrosion-resistant components |
| Standards Compliance | GB/T 2816-2014, GB/T 2818-2014 |
Applications and Use Cases
The versatility of the 175QJB pump makes it suitable for a wide range of applications, including:
- Industrial Water Supply: Providing reliable water sources for manufacturing processes, cooling systems, and boiler operations.
- Agricultural Irrigation: Efficiently extracting water from deep wells to support large-scale farming operations.
- Municipal Water Management: Ensuring a steady supply of water for urban areas, particularly in regions with limited surface water resources.
- Geological and Mining Operations: Removing groundwater from excavation sites to prevent flooding and ensure safe working conditions.
Its ability to operate in extreme conditions and its compliance with international standards make it a preferred choice for critical applications where reliability is paramount.
Company Background: Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd.
Hebei Aochite is a leading manufacturer of water supply and drainage equipment, with a strong focus on innovation and quality. The company's expertise in OEM processing allows it to cater to diverse market demands, offering customized solutions for both domestic and international clients. With a dedicated team of engineers and technicians, Hebei Aochite ensures that its products meet the highest standards of performance and safety.
As highlighted in NIST's mission to advance technology through precise measurements and standards, Hebei Aochite aligns its manufacturing processes with similar principles. The company's adherence to GB/T standards reflects its commitment to quality, ensuring that its products are not only efficient but also compliant with national and international regulations.
Conclusion
The 175QJB Deep Well Submersible Pump exemplifies the synergy between advanced engineering and rigorous quality control. Its robust design, customization options, and compliance with industry standards make it a reliable solution for deep well water extraction. Hebei Aochite's dedication to innovation and customer-centric approaches further solidifies its position as a trusted provider in the water management sector.
As technology continues to evolve, the importance of standards set by organizations like the National Institute of Standards and Technology (NIST) becomes increasingly evident. These standards not only ensure product reliability but also drive the development of safer, more efficient solutions for global challenges.
References
National Institute of Standards and Technology (NIST). (n.d.). Driving Innovation. Retrieved from https://www.nist.gov
Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd.. (n.d.). Product Specifications. Retrieved from https://www.wellpumpact.com
-
Efficient High Performance 1.5 hp deep well water pump Guide
NewsJul.01,2026
-
Choosing the Best 1 hp Vertical Deep Well Pump for Water Supply
NewsJun.29,2026
-
Best 1 hp deep well submersible pump for Water Supply
NewsJun.27,2026
-
Efficient 1 2 hp 5 gpm submersible well pump for Home and Farm
NewsJun.26,2026
-
Best 1 1 2 hp Deep Well Submersible Pump for Water Supply
NewsJun.25,2026
-
Troubleshooting Guide for Submersible Pump Not Working Properly
NewsJun.23,2026
-
 Efficient High Performance 1.5 hp deep well water pump GuideMaximizing Water Efficiency with a 1.5 hp Deep Well Water Pump Finding a reliable water source from deep underground requires precision engineering and robust power. The 1.5 hp deep well water pump offers the perfect balance of energy efficiency and high-performance output for various residential and agricultural needs. Whether you are managing a farm, supplying water to a high-rise building, or ensuring a steady flow for domestic use, selecting the right submersible pump is critical to avoid system failure and costly repairs. In this comprehensive guide, we will explore the technical advantages, installation best practices, and the operational versatility of these specialized pumping systems.Detail
-
 Choosing the Best 1 hp Vertical Deep Well Pump for Water SupplyEnsuring a reliable water supply from deep underground requires precision engineering and the right equipment. The 1 hp vertical deep well pump is a cornerstone for residential and small-scale agricultural water extraction, blending efficiency with powerful lifting capabilities. Whether you are managing a domestic water system, irrigating a garden, or extracting water from a river, selecting a pump with a water-immersed motor ensures long-term durability without water pollution. In this comprehensive guide, we will explore the technical advantages, installation requirements, and maintenance tips to maximize your pumps lifespan.Detail
-
 Best 1 hp deep well submersible pump for Water SupplyChoosing the Best 1 hp Deep Well Submersible Pump for Your Water Needs Finding a reliable water source often requires professional equipment capable of lifting water from significant depths. The 1 hp deep well submersible pump is a versatile and powerful solution designed for residential, agricultural, and industrial applications. By integrating high-quality silicon steel and waterproof motor windings, these pumps ensure longevity and efficiency even in demanding environments. Whether you are managing a farm, supplying a high-rise building, or securing domestic water, understanding the technical nuances of these pumps is key to maximizing your systems lifespan.Detail
 Afrikaans
 Albanian
 Amharic
 Arabic
 Armenian
 Azerbaijani
 Basque
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Catalan
 Cebuano
 Corsican
 Croatian
 Czech
 Danish
 Dutch
 Esperanto
 Estonian
 Finnish
 French
 Frisian
 Galician
 Georgian
 German
 Greek
 Gujarati
 Haitian Creole
 Hausa
 Hawaiian
 Hebrew
 Hindi
 Miao
 Hungarian
 Icelandic
 Igbo
 Indonesian
 Irish
 Italian
 Japanese
 Javanese
 Kannada
 Kazakh
 Khmer
 Rwandese
 Korean
 Kurdish
 Kyrgyz
 Lao
 Latin
 Latvian
 Lithuanian
 Luxembourgish
 Macedonian
 Malgashi
 Malay
 Malayalam
 Maltese
 Maori
 Marathi
 Mongolian
 Myanmar
 Nepali
 Norwegian
 Norwegian
 Occitan
 Pashto
 Persian
 Polish
 Portuguese
 Punjabi
 Romanian
 Russian
 Samoan
 Scottish Gaelic
 Serbian
 Sesotho
 Shona
 Sindhi
 Sinhala
 Slovak
 Slovenian
 Somali
 Spanish
 Sundanese
 Swahili
 Swedish
 Tagalog
 Tajik
 Tamil
 Tatar
 Telugu
 Thai
 Turkish
 Turkmen
 Ukrainian
 Urdu
 Uighur
 Uzbek
 Vietnamese
 Welsh
 Bantu
 Yiddish
 Yoruba
 Zulu
 English