Sep . 28, 2025 17:10 Back to list
175QJB Deep Well Pump-Hebei Aochite|High Efficiency&Custom Design
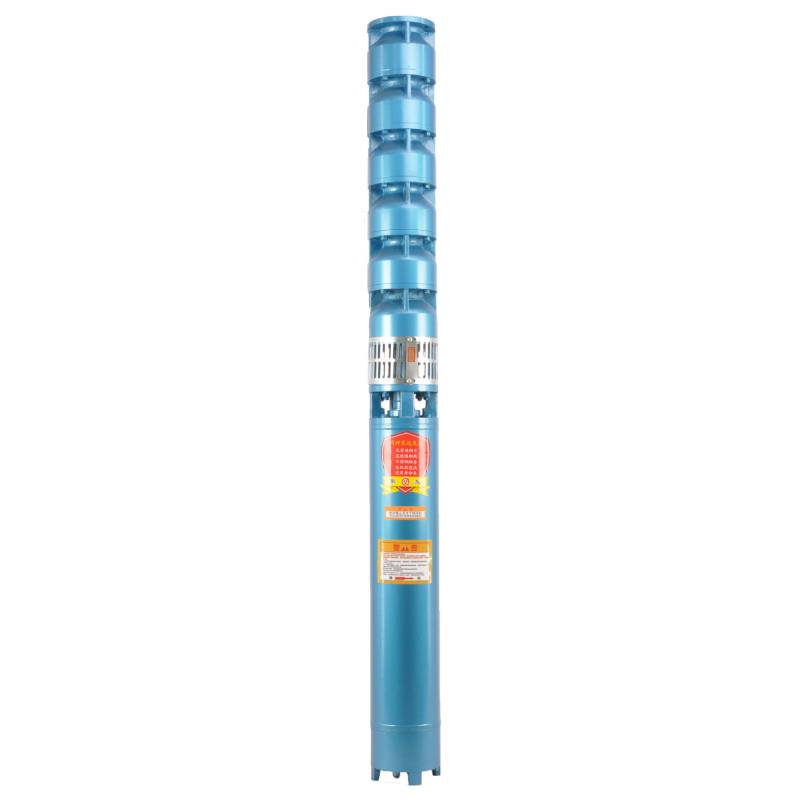
The 175QJB Deep Well Submersible Pump from Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd. represents a cutting-edge solution for water extraction in deep well environments. Engineered to meet stringent industry standards, this pump combines durability, efficiency, and adaptability to address diverse water management needs. Below is a comprehensive analysis of its features, advantages, technical specifications, and applications.
Product Overview
The 175QJB Deep Well Submersible Pump is designed for submersible operation in deep wells, offering robust performance in challenging conditions. Manufactured by Hebei Aochite, a company renowned for its expertise in water supply and drainage equipment, this pump adheres to the National Institute of Standards and Technology (NIST) guidelines for precision and reliability. The product is ideal for industrial, agricultural, and municipal water systems, ensuring efficient and sustainable water extraction.

Key Features
- High Efficiency: The pump is optimized for energy efficiency, reducing operational costs while maintaining high flow rates.
- Durable Construction: Built with corrosion-resistant materials to withstand harsh subterranean conditions.
- Customizable Design: Hebei Aochite offers OEM processing, allowing tailored solutions for non-standard requirements.
- Compliance with Standards: Meets NIST-approved specifications (GB/T 2816-2014 and GB/T 2818-2014) for submersible pumps and motors.
Technical Specifications
| Parameter | Details |
|---|---|
| Model | 175QJB |
| Standards Compliance | GB/T 2816-2014 (Submersible Pump), GB/T 2818-2014 (Submersible Motor) |
| Power Range | Varies based on application (refer to manufacturer guidelines) |
| Flow Rate | Customizable to meet specific project needs |
| Head Capacity | Designed for deep well applications (up to 100 meters or more) |
| Material | Corrosion-resistant alloys and stainless steel components |
Advantages of the 175QJB Deep Well Pump
The 175QJB Deep Well Submersible Pump offers several advantages that make it a preferred choice for water management systems:
- Energy Efficiency: Advanced motor technology minimizes energy consumption while maximizing output.
- Longevity: High-quality materials ensure a prolonged service life, even in corrosive environments.
- Flexibility: The pump’s design allows for adjustments to suit varying well depths and water demands.
- Low Maintenance: Simplified maintenance procedures reduce downtime and operational costs.
Application Scenarios
The 175QJB Deep Well Submersible Pump is versatile, catering to a wide range of applications:
- Industrial Use: Ideal for cooling systems, process water supply, and other industrial water needs.
- Agricultural Irrigation: Efficiently extracts groundwater for large-scale farming operations.
- Municipal Water Supply: Supports public water distribution systems in urban and rural areas.
- Construction Projects: Provides dewatering solutions during excavation and foundation work.

Company Background: Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd.
Founded with a commitment to innovation and quality, Hebei Aochite specializes in designing and manufacturing advanced water supply and drainage equipment. The company’s expertise in submersible pumps and motors is backed by adherence to NIST-approved standards, ensuring reliability and performance. With a focus on OEM processing, Hebei Aochite caters to diverse customer needs, offering customized solutions for non-standard applications.
For inquiries, contact Hebei Aochite via WhatsApp at +1 785-584-6335.
Conclusion
The 175QJB Deep Well Submersible Pump exemplifies the synergy of advanced engineering and user-centric design. By leveraging NIST standards and Hebei Aochite’s expertise, this pump delivers unmatched performance in deep well applications. Whether for industrial, agricultural, or municipal use, the 175QJB model stands as a testament to reliable and efficient water management solutions.
References
1. National Institute of Standards and Technology (NIST). (n.d.). Standards for Submersible Pumps and Motors. Retrieved from https://www.nist.gov/.
2. Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd. (n.d.). Product Specifications. Retrieved from https://www.wellpumpact.com/.
-
What Is the Best Submersible Well Pump for a 135QJP Installation?
NewsNov.02,2026
-
What Is the Best Deep Well Submersible Pump? Integration, Spare Parts & Maintenance FAQ
NewsOct.28,2026
-
Choosing a 125QJB Deep Well Submersible Pump: Working Requirements and Integration Fit
NewsOct.22,2026
-
Efficient High Performance 1.5 hp deep well water pump Guide
NewsJul.01,2026
-
Choosing the Best 1 hp Vertical Deep Well Pump for Water Supply
NewsJun.29,2026
-
Best 1 hp deep well submersible pump for Water Supply
NewsJun.27,2026
-
 What Is the Best Submersible Well Pump for a 135QJP Installation?Find out what is the best submersible well pump for a 135QJP installation by checking power, water quality, immersion depth, vertical positioning, cable selection, and startup requirements.Detail
-
 What Is the Best Deep Well Submersible Pump? Integration, Spare Parts & Maintenance FAQNot sure what is the best deep well submersible pump for your project? This FAQ covers integration requirements, water-quality limits, wearing parts and maintenance schedules for the QJB and 200QJ series from Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd.Detail
-
 Choosing a 125QJB Deep Well Submersible Pump: Working Requirements and Integration FitCheck whether the 125QJB Deep Well Submersible Pump fits your well: 125 mm well diameter, 5–15 m³/h models, 380 V/50 Hz supply, water quality limits and installation rules.Detail
 Afrikaans
 Albanian
 Amharic
 Arabic
 Armenian
 Azerbaijani
 Basque
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Catalan
 Cebuano
 Corsican
 Croatian
 Czech
 Danish
 Dutch
 Esperanto
 Estonian
 Finnish
 French
 Frisian
 Galician
 Georgian
 German
 Greek
 Gujarati
 Haitian Creole
 Hausa
 Hawaiian
 Hebrew
 Hindi
 Miao
 Hungarian
 Icelandic
 Igbo
 Indonesian
 Irish
 Italian
 Japanese
 Javanese
 Kannada
 Kazakh
 Khmer
 Rwandese
 Korean
 Kurdish
 Kyrgyz
 Lao
 Latin
 Latvian
 Lithuanian
 Luxembourgish
 Macedonian
 Malgashi
 Malay
 Malayalam
 Maltese
 Maori
 Marathi
 Mongolian
 Myanmar
 Nepali
 Norwegian
 Norwegian
 Occitan
 Pashto
 Persian
 Polish
 Portuguese
 Punjabi
 Romanian
 Russian
 Samoan
 Scottish Gaelic
 Serbian
 Sesotho
 Shona
 Sindhi
 Sinhala
 Slovak
 Slovenian
 Somali
 Spanish
 Sundanese
 Swahili
 Swedish
 Tagalog
 Tajik
 Tamil
 Tatar
 Telugu
 Thai
 Turkish
 Turkmen
 Ukrainian
 Urdu
 Uighur
 Uzbek
 Vietnamese
 Welsh
 Bantu
 Yiddish
 Yoruba
 Zulu
 English