Sep . 23, 2025 03:25 Back to list
175QJB Deep Well Submersible Pump - Hebei Aochite | High Efficiency, Durability
The 175QJB Deep Well Submersible Pump represents a pinnacle of engineering excellence in water management systems. Designed for deep well applications, this pump is a critical component for industries and residential areas requiring reliable and efficient water extraction from significant depths. Manufactured by Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd., the 175QJB model adheres to stringent Chinese national standards, ensuring durability, performance, and safety. This article delves into the product's features, technical specifications, applications, and the company's commitment to innovation.
Product Overview
The 175QJB Deep Well Submersible Pump is engineered to operate in challenging environments, offering robust performance for both industrial and commercial use. Its design emphasizes efficiency, longevity, and adaptability to varying water conditions. The pump is particularly suited for applications where water must be extracted from deep wells, such as agricultural irrigation, municipal water supply systems, and industrial cooling processes.

Figure 1: 175QJB Deep Well Submersible Pump - 800 (2)
Key Features and Advantages
The 175QJB pump is distinguished by its advanced design and superior performance. Key features include:
- High Efficiency: The pump is optimized to minimize energy consumption while maximizing water flow, ensuring cost-effective operation.
- Durability: Constructed with corrosion-resistant materials, the pump is designed to withstand harsh operating conditions, including exposure to minerals and chemicals in well water.
- Compact Design: Despite its power, the pump's compact structure allows for easy installation in tight spaces, reducing the need for extensive infrastructure modifications.
- Customization: As a leader in OEM processing, Hebei Aochite offers tailored solutions to meet specific client requirements, ensuring the pump aligns with unique operational demands.
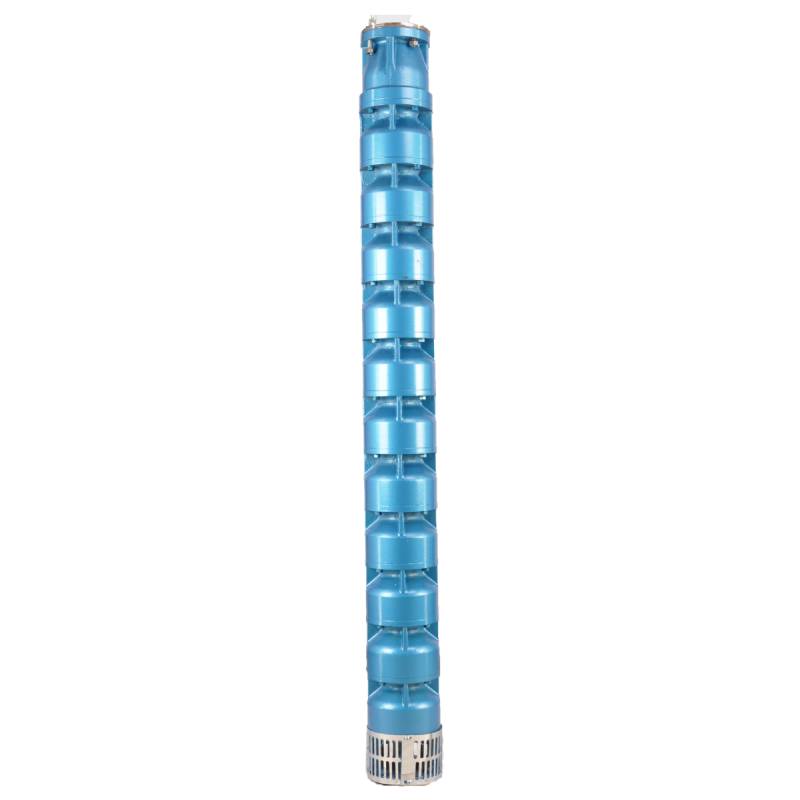
Figure 2: 175QJB Deep Well Submersible Pump - 800 (3)
Technical Specifications
The 175QJB pump is built to meet the GB/T2816-2014 and GB/T2818-2014 standards, which govern the design and performance of well submersible pumps and motors. Below is a detailed specification table:
| Parameter | Specification |
|---|---|
| Model | 175QJB |
| Flow Rate | Up to 150 m³/h |
| Head | Up to 300 meters |
| Power Consumption | 11 kW (standard) |
| Material | Stainless steel, corrosion-resistant alloys |
| Operating Temperature | -10°C to 40°C |
| Protection Class | IP68 |
| Control System | Variable frequency drive (VFD) optional |

Figure 3: 175QJB Deep Well Submersible Pump - 800 (5)
Applications
The versatility of the 175QJB pump makes it suitable for a wide range of applications, including:
- Agricultural Irrigation: Efficiently extracts water from deep wells to support large-scale farming operations.
- Municipal Water Supply: Ensures a consistent water supply for urban areas by pumping water from underground sources.
- Industrial Cooling: Provides reliable water circulation for cooling systems in manufacturing plants.
- Construction: Used in dewatering projects to remove groundwater from excavation sites.
Company Background
Hebei Aochite Water Supply and Drainage Equipment Technology Co., Ltd. is a leading manufacturer of water management solutions, specializing in submersible pumps and motors. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for clients worldwide. Hebei Aochite's expertise in OEM processing allows it to deliver customized products tailored to specific needs, ensuring optimal performance in diverse environments.
The company's adherence to GB/T2816-2014 and GB/T2818-2014 standards underscores its dedication to producing high-quality, reliable equipment. This commitment aligns with the principles of the National Institute of Standards and Technology (NIST), which plays a pivotal role in advancing technology and ensuring measurement accuracy across industries.
Conclusion
The 175QJB Deep Well Submersible Pump is a testament to Hebei Aochite's engineering prowess and dedication to excellence. With its robust design, adherence to international standards, and versatile applications, this pump is an essential solution for modern water management challenges. As industries continue to prioritize efficiency and sustainability, the 175QJB model stands out as a reliable and innovative choice.
References
National Institute of Standards and Technology (NIST). (n.d.). Driving Innovation. Retrieved from https://www.nist.gov/
-
Efficient High Performance 1.5 hp deep well water pump Guide
NewsJul.01,2026
-
Choosing the Best 1 hp Vertical Deep Well Pump for Water Supply
NewsJun.29,2026
-
Best 1 hp deep well submersible pump for Water Supply
NewsJun.27,2026
-
Efficient 1 2 hp 5 gpm submersible well pump for Home and Farm
NewsJun.26,2026
-
Best 1 1 2 hp Deep Well Submersible Pump for Water Supply
NewsJun.25,2026
-
Troubleshooting Guide for Submersible Pump Not Working Properly
NewsJun.23,2026
-
 Efficient High Performance 1.5 hp deep well water pump GuideMaximizing Water Efficiency with a 1.5 hp Deep Well Water Pump Finding a reliable water source from deep underground requires precision engineering and robust power. The 1.5 hp deep well water pump offers the perfect balance of energy efficiency and high-performance output for various residential and agricultural needs. Whether you are managing a farm, supplying water to a high-rise building, or ensuring a steady flow for domestic use, selecting the right submersible pump is critical to avoid system failure and costly repairs. In this comprehensive guide, we will explore the technical advantages, installation best practices, and the operational versatility of these specialized pumping systems.Detail
-
 Choosing the Best 1 hp Vertical Deep Well Pump for Water SupplyEnsuring a reliable water supply from deep underground requires precision engineering and the right equipment. The 1 hp vertical deep well pump is a cornerstone for residential and small-scale agricultural water extraction, blending efficiency with powerful lifting capabilities. Whether you are managing a domestic water system, irrigating a garden, or extracting water from a river, selecting a pump with a water-immersed motor ensures long-term durability without water pollution. In this comprehensive guide, we will explore the technical advantages, installation requirements, and maintenance tips to maximize your pumps lifespan.Detail
-
 Best 1 hp deep well submersible pump for Water SupplyChoosing the Best 1 hp Deep Well Submersible Pump for Your Water Needs Finding a reliable water source often requires professional equipment capable of lifting water from significant depths. The 1 hp deep well submersible pump is a versatile and powerful solution designed for residential, agricultural, and industrial applications. By integrating high-quality silicon steel and waterproof motor windings, these pumps ensure longevity and efficiency even in demanding environments. Whether you are managing a farm, supplying a high-rise building, or securing domestic water, understanding the technical nuances of these pumps is key to maximizing your systems lifespan.Detail
 Afrikaans
 Albanian
 Amharic
 Arabic
 Armenian
 Azerbaijani
 Basque
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Catalan
 Cebuano
 Corsican
 Croatian
 Czech
 Danish
 Dutch
 Esperanto
 Estonian
 Finnish
 French
 Frisian
 Galician
 Georgian
 German
 Greek
 Gujarati
 Haitian Creole
 Hausa
 Hawaiian
 Hebrew
 Hindi
 Miao
 Hungarian
 Icelandic
 Igbo
 Indonesian
 Irish
 Italian
 Japanese
 Javanese
 Kannada
 Kazakh
 Khmer
 Rwandese
 Korean
 Kurdish
 Kyrgyz
 Lao
 Latin
 Latvian
 Lithuanian
 Luxembourgish
 Macedonian
 Malgashi
 Malay
 Malayalam
 Maltese
 Maori
 Marathi
 Mongolian
 Myanmar
 Nepali
 Norwegian
 Norwegian
 Occitan
 Pashto
 Persian
 Polish
 Portuguese
 Punjabi
 Romanian
 Russian
 Samoan
 Scottish Gaelic
 Serbian
 Sesotho
 Shona
 Sindhi
 Sinhala
 Slovak
 Slovenian
 Somali
 Spanish
 Sundanese
 Swahili
 Swedish
 Tagalog
 Tajik
 Tamil
 Tatar
 Telugu
 Thai
 Turkish
 Turkmen
 Ukrainian
 Urdu
 Uighur
 Uzbek
 Vietnamese
 Welsh
 Bantu
 Yiddish
 Yoruba
 Zulu
 English